Five-Profile Arc and Bevel Edge Bander, PUR
Five profiles on one bed, with PUR in two colours: 45° full bevel, 45° bevel-straight, quarter-round, half-round and duck-bill, bonded with an adhesive that survives a wet kitchen and a dark decor.
Overview
PUR is usually specified for one of two reasons: the panel is going into a wet or hot environment, or the decor is dark or high-gloss, where an EVA line slowly shows through. On a curved door both reasons apply at the bevel and at the arc, so the glue decision has to be made for the whole profile set rather than for one straight edge.
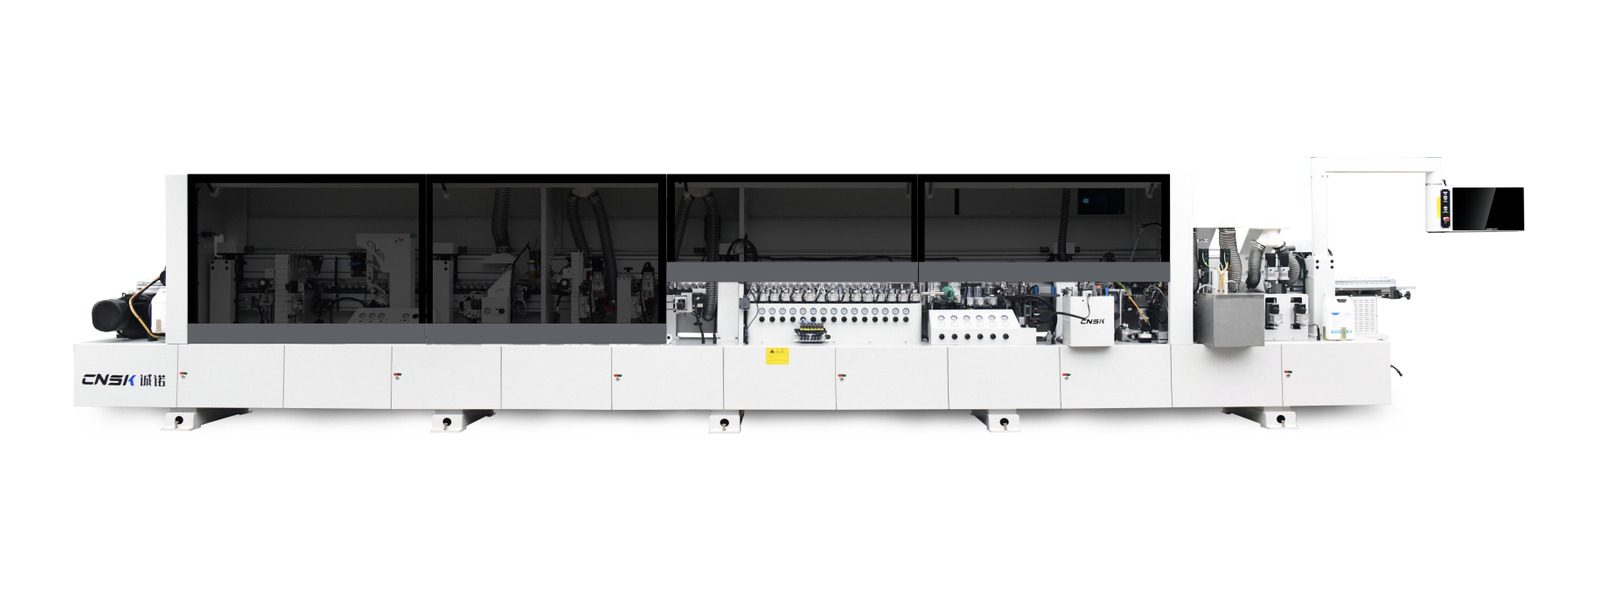
This machine takes the profile set of the FM725YCX and runs it on a no-cleaning PUR pot that switches between two colours. The 45° bevel is glued and pressed in one servo-controlled pass, the band is grooved before it goes round the corner, and the same bed carries the quarter-round, half-round and duck-bill formats a curved-door programme needs.
Station sequence
Twenty stations behind the screen, from the separating spray to the servo polishing head, in the order the panel runs.
Technical data
| Model | FM726YCX |
| Total power | 44.1 kW |
| Voltage | 380 V |
| Air pressure | 0.7 MPa |
| Electric lift | Motorized |
| Feed speed | 5 m/min · 8 m/min on 45° bevel-straight |
| Panel width | ≥ 120 mm |
| Machine size (L × W × H) | 9350 × 950 × 1700 mm |
| Machine weight | 3600 kg |
| Panel thickness · 45° full bevel | 9 – 22 mm |
| Panel thickness · 45° bevel-straight | 9 – 25 mm |
| Panel thickness · 1/4 arc | 18 – 22 mm |
| Panel thickness · 1/2 arc | 18 – 22 mm |
| Panel thickness · duck-bill | 18 – 22 mm |
| Edge band thickness · 45° full bevel | 0.8 – 1.0 mm |
| Edge band thickness · 45° bevel-straight | 0.8 – 1.0 mm |
| Edge band thickness · 1/4 arc | 0.6 – 0.8 mm |
| Edge band thickness · 1/2 arc | 0.6 – 0.8 mm |
| Edge band thickness · duck-bill | 0.6 – 0.8 mm |
| Edge band width · 45° full bevel | 30 mm |
| Edge band width · 45° bevel-straight | 30 mm |
| Edge band width · 1/4 arc | 40 mm |
| Edge band width · 1/2 arc | 40 mm |
| Edge band width · duck-bill | 40 mm |
Figures are taken from the FM726YCX PUR technical data sheet in the 2026 configuration list. Panel thickness, edge band thickness and edge band width are stated per profile; the tooling set for each profile is confirmed against your door drawings before the offer is issued.
What the machine is built to do
- Five profiles on one bed45° full bevel, 45° bevel-straight, quarter-round, half-round and duck-bill are all available on the same bed; the recipe decides which units run.
- Two-colour PUR, no cleaningA no-cleaning PUR pot holds two adhesive colours and switches between them without a solvent flush, so a colour change is a recipe change rather than a teardown.
- 45° glued and pressed in one passThe bevel is glued and laminated at the same station under servo control, which is what keeps a full-bevel joint invisible on a dark panel.
- Grooving before the cornerThe band is grooved on its inner face before it is pressed round the corner, so the 45° return stays sharp instead of lifting.
- Servo press-fitting on the profileThe pressing module follows the contour of the shaped panel, so the band seats along the curve instead of being loaded flat across it.
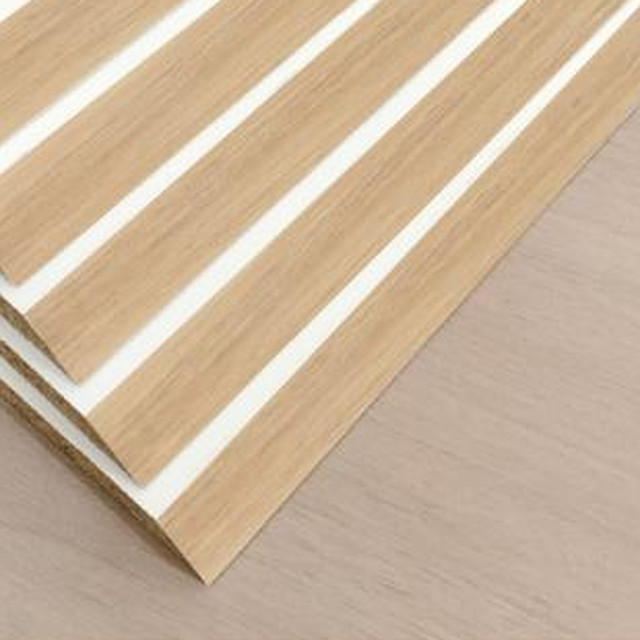
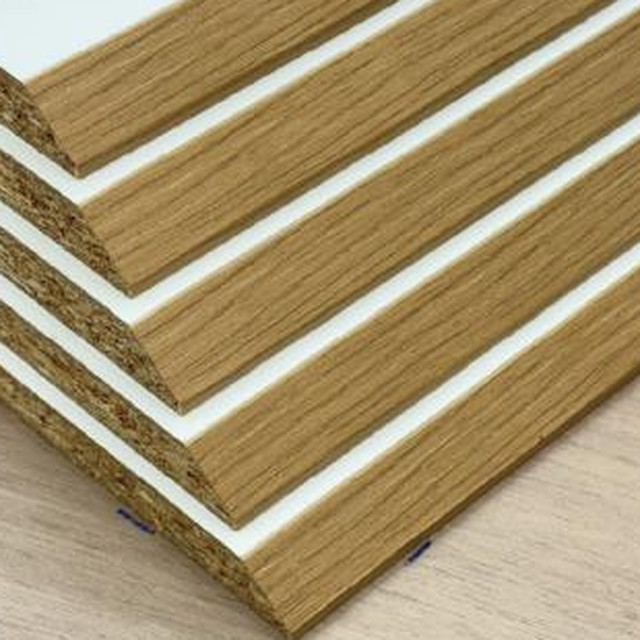
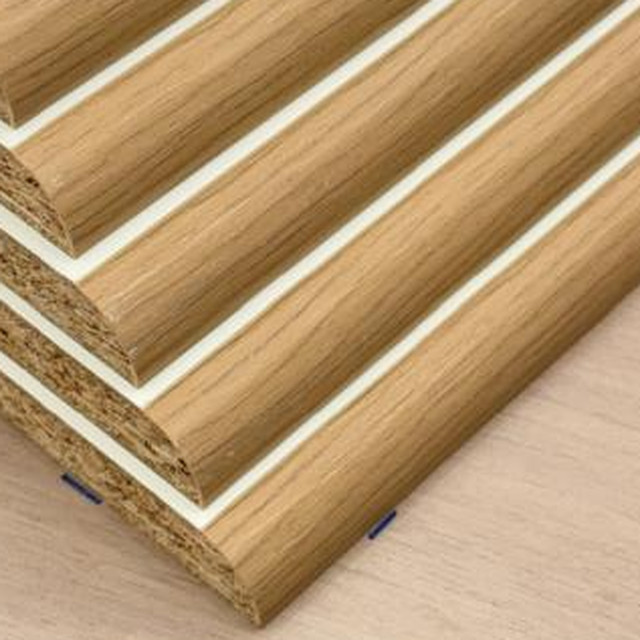
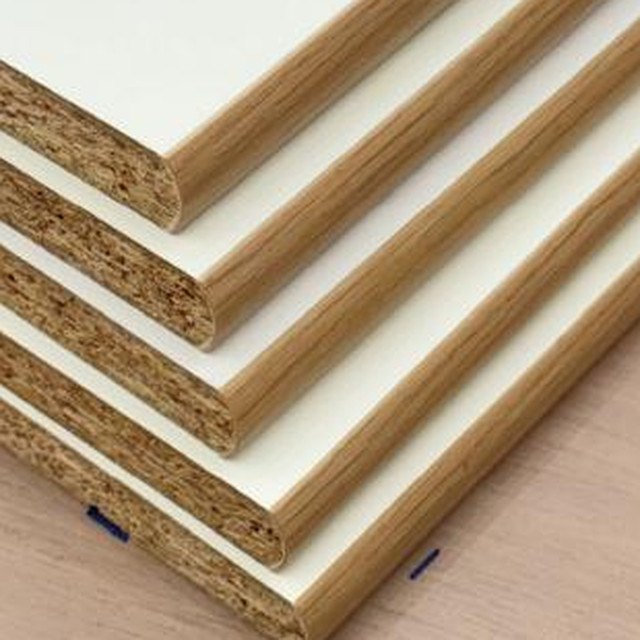
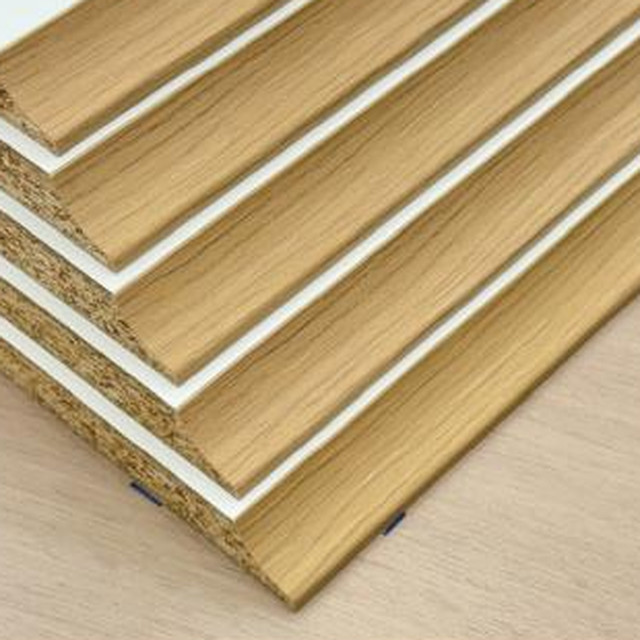
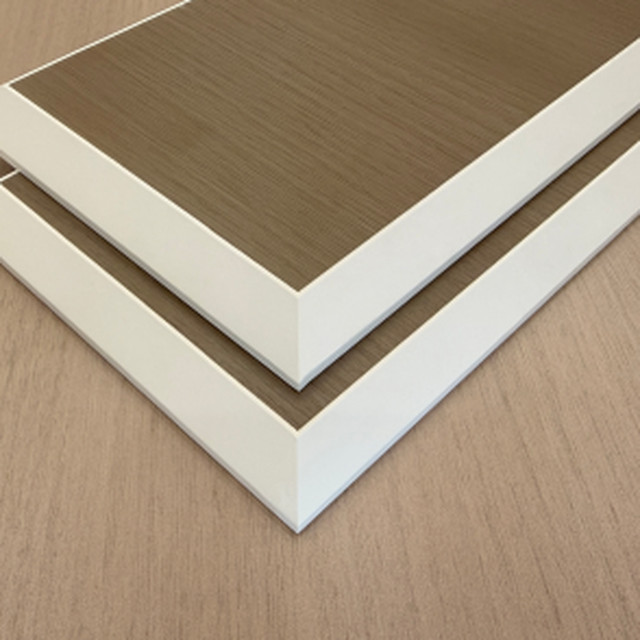
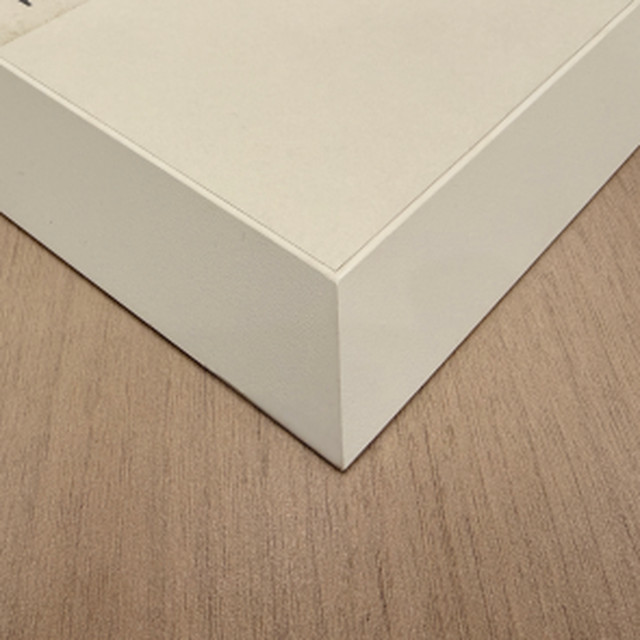
Edge samples
More from the 7 series
Double-Layer Handle-Free Edge Bander
Thirty handle-free profiles on one machine, switched from the screen with no waiting between shapes.
45° Bevel and Straight Edge Bander
The 45° bevel and the straight edge finished on the same line, plus soft-forming for wrapped profiles.
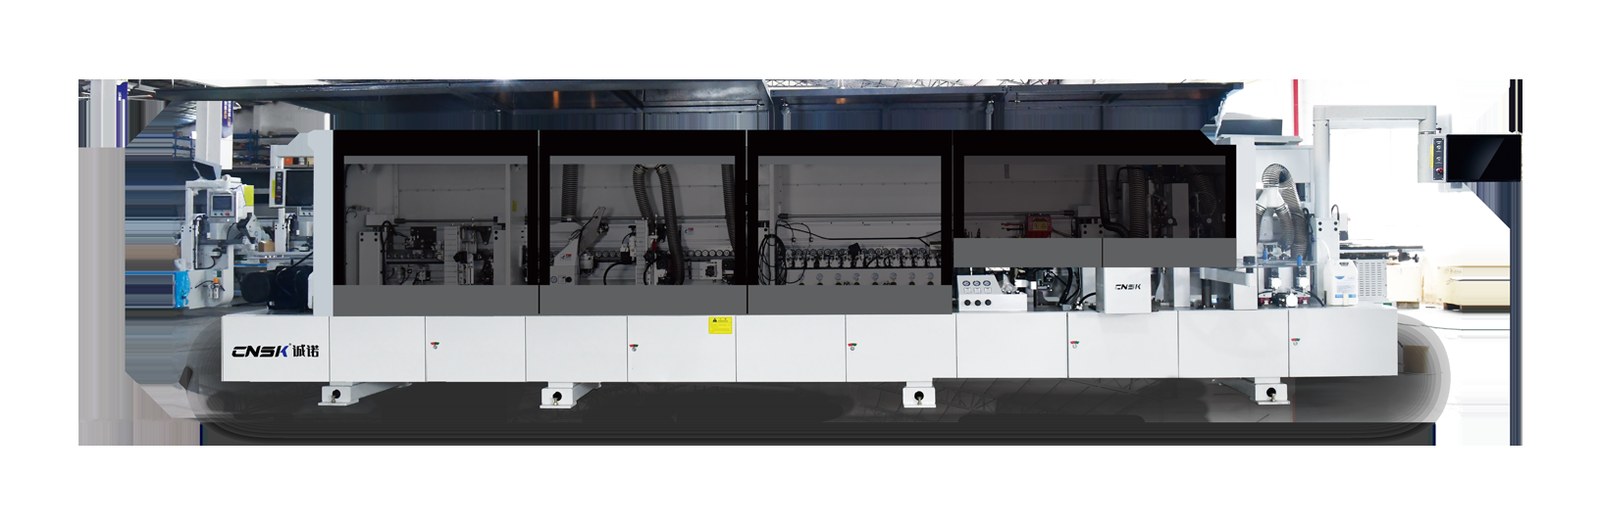
Five-Profile Arc and Bevel Edge Bander
Half-round, quarter-round, 45° bevel-straight, full bevel and duck-bill — five profiles on one bed.
Put FM726YCX against your panel.
Send the thickness, width and band you run. You get a station list, the tooling and a price against your name.